
Some of the most dependable metal products around us began as rough, hot-rolled material and were transformed into something remarkably smooth, strong, and precise. That transformation has a name: cold rolling. It is one of the most widely used ways to give metal sheet, strip, and bar the accuracy, finish, and strength that modern industry expects.
For manufacturers and buyers across the UAE, understanding cold rolling helps you choose the right material, set realistic expectations, and avoid surprises later on. In this guide, we’ll walk through how it works, what it does to the metal, where it shines, and where its limits are, all in plain, practical language.
What Is Cold Rolling?
Cold rolling is a metalworking process in which metal is passed through rollers at or near room temperature, below its recrystallisation temperature, to reduce its thickness and improve its properties. Because the metal is not heated, it keeps its shape more precisely and develops a smoother surface and higher strength than it would through hot working.
Understanding the Cold Rolling Process
In the cold rolling process, a piece of metal, usually in coil form, is squeezed between rotating rolls under high pressure. Each pass reduces the thickness a little and lengthens the metal. The result is a product with tighter tolerances, a cleaner surface, and improved mechanical properties.
What Is Cold Rolled Steel?
Cold rolled steel is steel that has first been hot rolled, cleaned of scale, and then reduced further at room temperature. It is commonly supplied as sheet, strip, and coil, and cold-finished bars are also widely used in engineering. Compared with hot-rolled steel, it offers a smoother surface, closer dimensional control, and greater strength, which is why it is a popular choice for visible, precise, and high-performance parts.
How Does the Cold Rolling Process Work?
While the equipment can be sophisticated, the sequence itself is straightforward.
Step 1: Preparing the Metal
The starting material is usually hot-rolled coil. It is cleaned, often by pickling in acid, to remove the oxide scale left over from hot rolling. A clean surface is essential, because any scale or contamination pressed into the metal would show up in the finished product.
Step 2: Feeding the Material Through the Rollers
The cleaned coil is fed into a rolling mill, which may be a single reversing mill or a series of stands arranged in tandem. Work rolls apply the pressure, supported by larger backup rolls that keep them rigid. A rolling lubricant is used to control friction and heat.
Step 3: Controlling Thickness Reduction
The metal is reduced in thickness over one or several passes. Operators and automated gauge control systems adjust roll gap and tension to hit the target thickness. Overall reductions commonly fall in the range of about 50 to 90 percent, depending on the material and the final requirement.
Step 4: Annealing When Required
Cold working makes metal harder and less ductile. If the product needs to be softer or more formable, it is annealed, meaning heated and cooled under control, to restore ductility. Many products are also given a light final pass, known as temper rolling or skin passing, to improve flatness and surface finish.
Step 5: Final Finishing and Inspection
The finished material is slitted, cut to length, oiled or coated as required, and inspected for thickness, flatness, surface quality, and mechanical properties before it is packed and shipped.
What Happens to Metal During Cold Rolling?
It helps to picture what is happening inside the metal, because that explains most of its behaviour.
Plastic Deformation and Grain Structure
As the metal is squeezed, it deforms permanently. Its internal grains become flattened and elongated in the rolling direction, which creates a fine, directional structure.
Work Hardening
Deformation increases the number of dislocations in the crystal structure, and these make further movement more difficult. This effect, called work hardening or strain hardening, is the main reason cold-rolled metal is stronger and harder.
Changes in Mechanical Properties
Cold rolling typically increases yield strength, tensile strength, and hardness while reducing ductility and elongation. Properties can also vary a little depending on direction, which is why rolling direction matters for forming and bending operations.
What Are the Benefits of Cold Rolling?
The cold rolling benefits are practical, measurable, and easy to appreciate in everyday manufacturing.
1. Improved Surface Finish
Cold-rolled material has a smooth, clean, often bright surface that suits painting, plating, and coating very well.
2. Better Dimensional Accuracy
Tighter thickness and width tolerances make it easier to design, fabricate, and assemble parts consistently.
3. Increased Strength and Hardness
Work hardening raises strength without the need for added alloying elements, so you get more performance from the same grade.
4. Improved Thickness Uniformity
Modern mills monitor and adjust thickness continuously, producing a very even gauge along the length and width of the material.
5. Better Surface Consistency
Fewer scale marks and surface irregularities mean a more predictable appearance and performance from coil to coil.
6. Flexible Mechanical Property Control
By combining the amount of reduction with annealing, producers can create a range of tempers, from soft and formable to full hard, to match the end use.
Cold Rolling vs Hot Rolling: What Is the Difference?
Hot rolling is done above the metal’s recrystallisation temperature, usually at very high heat for steel. Cold rolling is done at or near room temperature, usually on material that has already been hot rolled. They are complementary rather than competing, and each has its own sweet spot.
Key Differences Between Cold Rolling and Hot Rolling
| Factor | Cold Rolling | Hot Rolling |
| Processing Temperature | Room temperature or near | Above recrystallisation temperature |
| Surface Finish | Smooth, clean, bright | Rougher, with scale |
| Dimensional Accuracy | Tight tolerances | Looser tolerances |
| Strength and Hardness | Higher, due to work hardening | Lower |
| Ductility | Lower unless annealed | Higher |
| Typical Thickness | Thinner gauges | Thicker sections |
| Internal Stress | Higher residual stress | Lower |
| Cost | Higher, more processing steps | Generally lower |
When Should You Choose Cold Rolling?
Cold rolling is a great choice when you need:
- A fine surface for painting, plating, or visible parts
- Tight thickness and dimensional tolerances
- Higher strength in thinner sections
- Consistent quality for precision components
When Is Hot Rolling More Suitable?
Hot rolling is often the better fit for thick plates, structural sections, and large components where cost and ease of forming matter more than surface finish or tight tolerances.
Which Metals Can Be Cold Rolled?
Many metals respond well, particularly those with enough ductility to be deformed at room temperature.
Carbon and Alloy Steel
This is the most common group. Low-carbon steel is widely supplied as cold rolled steel sheet, strip, and bar, and alloy steels are cold rolled for stronger, more specialised applications.
Stainless Steel
Stainless steel is cold rolled to give a bright, corrosion-resistant finish and good strength. Austenitic grades work harden quickly, so mills use heavy equipment and careful annealing.
Aluminium and Aluminium Alloys
Aluminium is cold rolled into sheet, plate, and foil, with the amount of reduction helping to set the temper and strength.
Copper and Copper Alloys
Copper, brass, and bronze are cold rolled into strip and sheet used widely in electrical and decorative applications.
Nickel Alloys and Other Special Metals
Nickel alloys, titanium, and other special metals can be cold rolled too, though they usually need more powerful mills and more frequent annealing between stages.
What Are the Industrial Applications of Cold Rolling?
Oil and Gas Industry
Cold-rolled and cold-finished products are used in precision components, instrumentation parts, shims, gaskets, and equipment where dimensional accuracy and consistent properties are important.
Automotive Industry
Body panels, brackets, and structural parts rely on cold-rolled sheet for its excellent surface finish, formability, and strength.
Aerospace Industry
Aluminium, titanium, and nickel alloy sheet and foil are cold rolled to meet strict tolerance and property requirements.
Electrical and Electronics Industry
Silicon steel laminations for motors and transformers, along with copper strip and busbars, depend on the accuracy and surface quality of cold rolling.
Construction and Infrastructure
Roofing, cladding, framing, and light structural profiles all make good use of cold-rolled strip and sheet.
Industrial Machinery and Equipment
Shafts, pins, enclosures, and many precision parts begin as cold-rolled or cold-finished material, often followed by CNC machining to reach their final form. Because cold-rolled stock is consistent in size and finish, it machines predictably and is a popular starting point for accurate components.
What Are the Limitations of Cold Rolling?
Every process has trade-offs, and knowing them helps you plan well.
Reduced Ductility
Work hardening makes the metal stronger but less ductile, so severe bending or forming may need annealed material.
Residual Stress
Uneven deformation leaves internal stresses in the metal, which can cause movement during cutting, slitting, or CNC machining if not managed.
Higher Processing Requirements
Cold rolling needs powerful mills, careful lubrication, and often additional steps such as pickling and annealing, which adds time and cost.
Limitations in Thickness Reduction
There is a limit to how much the metal can be reduced before it becomes too hard and risks cracking. Thicker sections are generally better suited to hot rolling.
Surface Defects and Material Quality
Cold rolling can improve the surface, but it cannot hide serious defects in the starting material. Good incoming quality matters.
Additional Annealing Requirements
Where softness or high formability is needed, extra annealing steps are needed, which increases energy use and lead time.
Common Cold Rolling Defects and Their Causes
| Defect | What It Looks Like | Common Causes |
| Edge Cracking | Cracks along the strip edges | Low ductility, excessive reduction, edge flaws in the starting coil |
| Wavy Edges | Ripples along the edges | Edges elongate more than the centre, often from roll bending or crown issues |
| Centre Buckling | Waviness in the middle of the strip | Centre elongates more than the edges, often from uneven roll profile |
| Surface Scratches | Lines or marks on the surface | Damaged rolls, debris, or rough handling |
| Thickness Variation | Uneven gauge along or across the strip | Roll eccentricity, wear, or poor gauge control |
| Residual Stress Distortion | Bowing or warping after cutting | Uneven deformation leaving locked-in stress |
How to Prevent Common Cold Rolling Defects
The good news is that most defects can be prevented with disciplined practice:
- Inspect incoming material and reject coils with edge or surface flaws
- Control reduction per pass and use intermediate annealing when needed
- Maintain, grind, and replace rolls on schedule, and use correct roll profiles
- Filter and manage rolling lubricant to keep it clean
- Use automatic gauge and tension control to keep thickness uniform
- Apply levelling or stress-relief steps where distortion is a concern
What Is the Role of Annealing in Cold Rolling?
Why Does Cold-Rolled Metal Need Annealing?
As cold working continues, the metal gets harder and more brittle. Annealing heats it enough for new, stress-free grains to form, which restores ductility and softens the material so it can be formed or rolled further.
Intermediate vs Final Annealing
Intermediate annealing happens between rolling stages when the metal has become too hard to continue safely. Final annealing is carried out at the end to set the required softness, formability, and mechanical properties for the finished product.
Does All Cold-Rolled Steel Need Annealing?
No. Some products are intentionally supplied in the full-hard condition when high strength is needed and little forming is required. Others are annealed and skin passed for deep drawing and forming. The right choice depends on how the material will be used.
Read also: Preheating vs PWHT: Key Differences, Purposes and Applications
Cold Rolling Quality Control: What Should Manufacturers Check?
Thickness and Dimensional Tolerances
Thickness, width, and length should be checked against the specified tolerances using calibrated gauges and measuring equipment.
Surface Finish and Visual Inspection
The surface should be inspected for scratches, stains, roll marks, and other defects, and roughness can be measured where finish is critical.
Flatness and Shape Control
Flatness, camber, and edge waviness affect how well the material feeds into downstream equipment and how accurate the finished part is.
Mechanical Property Testing
Tensile, hardness, and bend tests confirm that strength, hardness, and ductility meet the required grade and temper.
Material Traceability and Specifications
Mill test certificates, heat numbers, and clear identification make sure every coil or bar can be traced back to its source and checked against the right standard.
Is Cold Rolling Suitable for Every Metal Product?
Not quite, but it suits a very wide range of them. Cold rolling is an excellent fit when you need accuracy, a fine finish, and good strength in thin to medium sections. It is less suitable for very thick sections, for applications where maximum ductility is needed without extra processing, or where cost is the only priority and finish and tolerance are not important. A short conversation about your application, material, and tolerances usually makes the best route clear.
Cold Rolling and CNC Machining with Accurate Edge
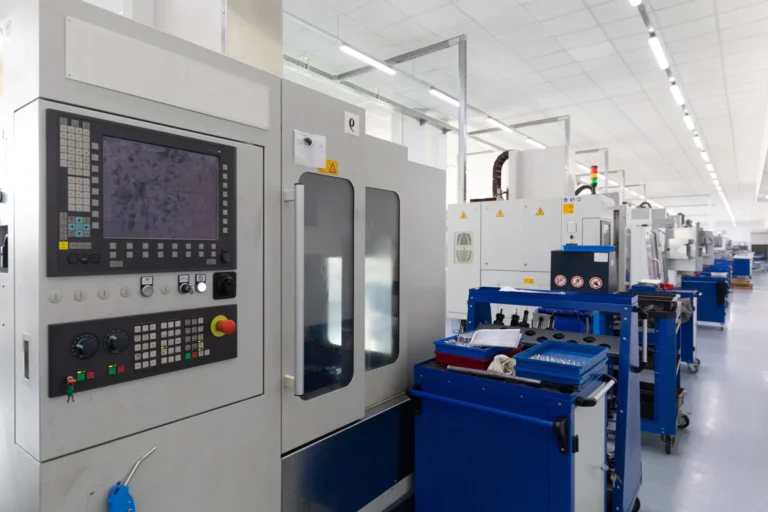
At Accurate Edge, we do cold rolling, and we pair it with CNC machining so your components can move smoothly from raw material to finished part. Our team helps you choose the right material, condition, and process for your application, with a focus on accuracy, consistency, and dependable delivery.
Get in touch to request a quotation or talk with our team about your next project. We would be delighted to help.
Conclusion
Cold rolling is a proven way to turn hot-rolled metal into material with a smoother surface, tighter tolerances, and higher strength. From cold rolled steel sheet to stainless, aluminium, and copper strip, it supports industries from oil and gas to automotive, aerospace, electronics, and construction. It does come with trade-offs, including reduced ductility, residual stress, and extra processing, but with good planning, annealing where needed, and solid quality control, those are all very manageable. Choose it where accuracy, finish, and strength matter, and you will get components that perform beautifully in service.
Frequently Asked Questions About Cold Rolling
What is cold rolling in simple terms?
It is a process where metal is passed through rollers at room temperature to make it thinner, smoother, and stronger, with better dimensional accuracy than hot-rolled material.
What is the difference between cold rolled and hot rolled steel?
Hot-rolled steel is processed at high temperature and has a rougher, scaled surface and looser tolerances. Cold rolled steel is processed further at room temperature, giving a smoother finish, tighter tolerances, and higher strength.
Is cold rolled steel stronger than hot rolled steel?
Generally yes, because work hardening increases its strength and hardness. The trade-off is lower ductility, unless the steel is annealed afterwards.
Does cold rolled steel need annealing?
Not always. Full-hard products are used as they are when high strength is needed, while annealed grades are supplied for applications that need more formability.
Is cold rolled steel good for CNC machining?
Yes. Its consistent size, smooth surface, and uniform properties make it a popular starting material for CNC machining. Stress-relieving or careful machining sequences can help control any movement caused by residual stress.
Which metals can be cold rolled?
Carbon and alloy steels, stainless steel, aluminium, copper and its alloys, and nickel alloys and other special metals can all be cold rolled.
What are the main cold rolling benefits?
The key benefits are a better surface finish, tighter dimensional accuracy, higher strength and hardness, uniform thickness, and the flexibility to control mechanical properties through reduction and annealing.